Medical product quality is more than a certificate in a supplier’s file. It affects whether a sterile dressing stays sealed, a diagnostic result is dependable, or a device performs as specified at a patient’s bedside. For global buyers, small differences in materials, manufacturing controls, and storage conditions can create real risks across long supply chains. Small details matter.
The World Health Organization’s 2017 Global Surveillance and Monitoring System report estimated that about one in ten medical products in low- and middle-income countries may be substandard or falsified. This estimate does not describe every product or market, but it shows why buyers need evidence beyond a low price or polished product page. A sensible review asks how to evaluate medical product quality through documented specifications, batch traceability, appropriate testing, packaging integrity, and clear instructions for use. Buyers should also check whether quality records match the exact product and manufacturing site being considered. Paperwork alone is not proof.
Reliable evaluation takes time. It may require technical review, supplier communication, and careful comparison of samples against stated requirements. No checklist catches everything; that is worth remembering. Still, a consistent process helps purchasing teams spot gaps before products reach clinics, distributors, or patients. Quality decisions are ultimately decisions about trust, performance, and patient safety.
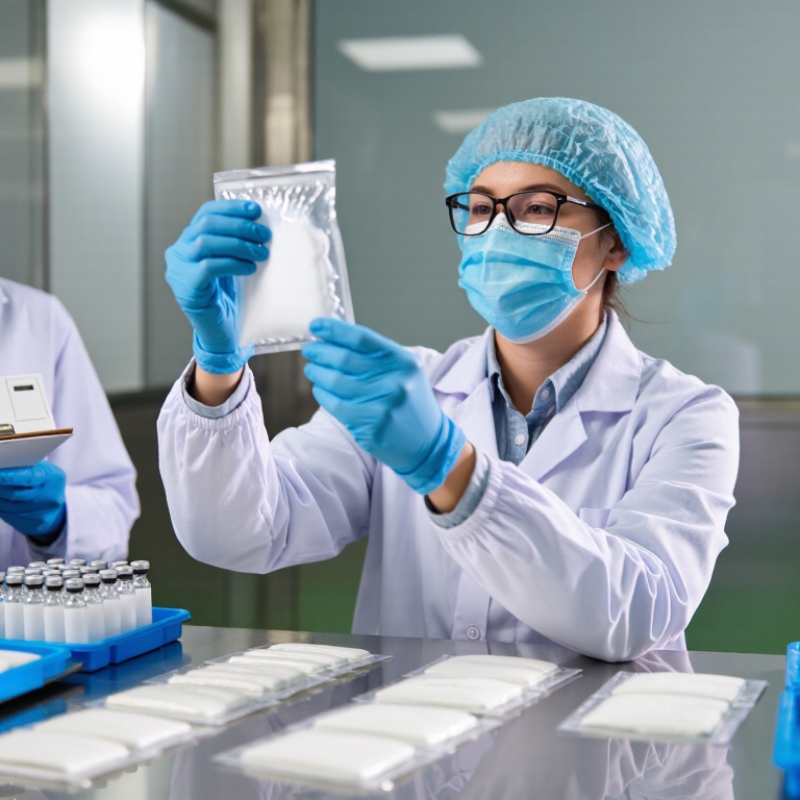
In global trade, medical product quality means more than a clean finish or convincing specification sheet. It means a product consistently performs as intended, from one production batch to the next. Buyers assess materials, dimensions, function, packaging, and the records that connect each shipment to its production history. A label that stays readable after handling matters. So does packaging that protects a sterile barrier during transport. Small details matter.
Quality must also travel across languages, climates, and supply chains. A buyer may review sample units, inspect production records, and compare test results with agreed requirements. Yet no document can replace careful checks of the actual product. That gap matters. Clear acceptance criteria, traceable batch records, and timely notice of changes help reduce uncertainty between supplier and buyer. Even then, quality is not a single perfect score; inspection methods can miss issues, and expectations may differ. Buyers should ask specific questions and keep reviewing performance after delivery, rather than treating approval as the end of the process.
| Quality Dimension | What It Means | Evidence Buyers Can Review | Why It Matters in Global Trade |
|---|---|---|---|
| Safety and risk control | Risks associated with intended use, foreseeable misuse, and the product lifecycle are identified and controlled. | Risk-management records, hazard controls, and applicable test reports. ISO 14971 describes a risk-management process for medical devices. | Supports patient and user protection and helps buyers assess whether risks have been addressed for the intended market and use. |
| Performance and consistency | The product performs as specified and maintains consistent characteristics across production batches. | Product specifications, verification and validation results, inspection records, and batch-release criteria. | Consistent performance reduces the risk of unsuitable or variable goods reaching healthcare providers in different markets. |
| Regulatory conformity | The product and its documentation meet the applicable rules in the destination market for its classification and intended purpose. | Market-specific registrations or authorizations, conformity documentation, labeling, and evidence required by the relevant regulator. | Requirements differ by jurisdiction and product type; conformity in one market does not automatically establish authorization in another. |
| Quality management system | Documented processes control design, purchasing, production, inspection, corrective action, and other relevant activities. | Quality-system procedures, audit information, and certification evidence where applicable. ISO 13485 specifies quality-management-system requirements for medical-device organizations. | A controlled system helps buyers evaluate how product quality is managed across suppliers and manufacturing stages; certification alone does not prove every product is compliant. |
| Materials and biological safety | Materials are suitable for the product’s design and intended contact with the body, where applicable. | Material specifications and a biological-evaluation rationale or test evidence appropriate to the device. The ISO 10993 series addresses biological evaluation of medical devices. | Material acceptability depends on factors such as contact type and duration; evidence should match the specific product and intended use. |
| Sterility and contamination control | For products supplied sterile, validated processes and packaging help establish and maintain the specified sterile state until use. | Sterilization validation, routine process records, packaging validation, and applicable shelf-life evidence. | Sterility is a product-specific requirement, not a feature of every medical product; buyers should verify claims and handling conditions for sterile goods. |
| Traceability and identification | Products and relevant production records can be linked to identifiers such as lot or serial numbers, where required. | Labeling samples, batch or serial records, and traceability procedures. Unique device identification requirements apply in certain jurisdictions and contexts. | Traceability supports distribution control, complaint investigation, and recall activities across borders. |
| Packaging, storage, and transport | Packaging and handling conditions protect the product during storage and shipment, including any specified temperature or humidity limits. | Packaging specifications, transport or distribution validation where appropriate, storage instructions, and temperature records when required. | Long international routes, customs delays, and climate differences can affect product condition if handling requirements are not controlled. |
| Labeling and instructions | Labels and instructions provide accurate, legible information needed for identification, safe use, storage, and applicable regulatory compliance. | Destination-market label and instruction samples, including language and symbol checks where relevant. | Language, labeling, and importer information requirements can vary by destination market and product category. |
| Post-market monitoring | Complaints, incidents, and product feedback are reviewed, investigated, and acted on through appropriate processes. | Complaint-handling procedures, investigation records, corrective-action processes, and applicable vigilance documentation. | Ongoing monitoring helps identify issues after distribution and supports timely action in the markets where the product is supplied. |
Note: Applicable standards and regulatory requirements depend on the product, its intended use, and the destination market. Buyers should confirm current requirements with the relevant regulatory authority or qualified regulatory professionals.
Buyers compare each production lot with defined specifications. Checks may cover dimensions, materials, labels, and performance. Numbers matter.
Testing can include functional trials, material analysis, and packaging inspections. For example, a sealed package may be checked after handling. Methods and acceptance limits should be clear.
Traceable records connect test results to specific lots. Buyers can review defects, complaints, and corrective actions over time. A neat report can still miss something.
No. Certificates can show that certain processes or facilities were reviewed, but they do not prove every unit performs well. Look at the evidence behind them.
Requirements depend on the product and destination market. Check classification, registration, labeling, language, and reporting obligations. Details change.
Request current specifications, test reports, and storage instructions. Confirm that documents match the exact product configuration, not a similar model. Ask how batches are identified.
A sample may show unclear markings, weak packaging, or confusing instructions. These small details matter. One sample cannot represent every unit.
Match labels and lot numbers with purchase records. Check seals, quantities, and visible damage; photograph anything unusual. Keep the notes.
Track complaints and returns by batch, then share specific findings with the supplier. Review handling and storage conditions too. Real shipments may expose gaps.
Medical product quality is essential in global trade because products must be safe, reliable, and consistent for patients and healthcare providers across different markets. It includes factors such as materials, performance, manufacturing controls, packaging, labeling, and the ability to remain effective during storage and transport. Buyers can assess quality through documented specifications, inspection results, testing data, and traceability records. International and regional standards provide shared frameworks for evaluating safety and performance, while local requirements may differ by destination.
Quality failures can cause patient harm, product recalls, delivery delays, and loss of confidence throughout supply chains. To understand how to evaluate medical product quality, buyers should review supplier capabilities, verify relevant certificates and test reports, inspect samples, and agree on clear acceptance criteria before purchasing. After delivery, they should monitor product condition, investigate complaints, and maintain records so potential issues can be identified and addressed promptly.
 RosMed Medical